TROUBLESHOOTING WELD LINES / FLOW MARKS IN INJECTION MOLDING
WELD LINES AND FLOW MARKS
MAJOR CAUSES FOR THE DEFECT :
- Molten plastic material is too cold in the mold after injection.
- when there is an excessive mold lubricant in the mold.
- Mold is too cold .
- Injection speed is slow.
- Low injection pressure.
- Volatile gas are been trapped in the mold.
- Air unable to escape from the mold as fast as it should.
TROUBLE SHOOTING :
- Increase injection pressure.
- Increase injection speed.
- Increase plasticizing capacity of machine if possible.
TEMPERATURE :
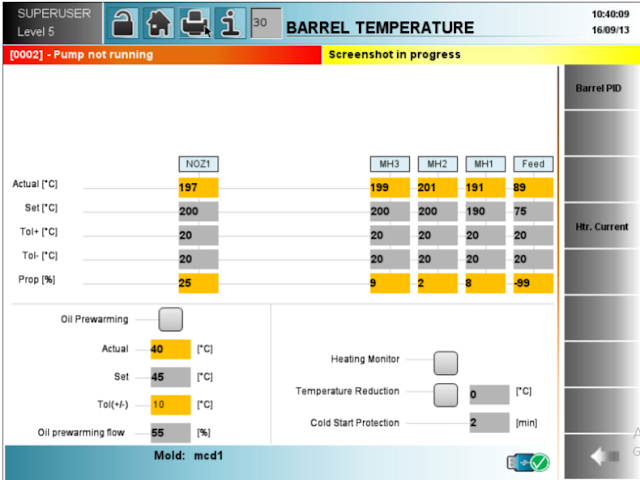
- Increase Barrel / Cylinder temperature.
- Increase Nozzle temperature.
- Increase Mold Temperature.
- Make proper/even/balanced cooling system for the mold.
MOLD :
- Add proper vent on the mold.
- Increase the runner system in the feed channel.
- Increase the gate system.
- Increase the opening of sprue.
- Make necessary adjustment for the mold adjustment.
- Thick the particular area where the welded part is too thin.
- Filling rate of the material in the mold should be equal.
- Increase the opening of nozzle.
- If the gate is too far from the weld one can add another substitute gate.
- Make necessary changes if wall thickness is too thin it will cause premature freezing.
- Check the core shifting if it has been done then make proper changes over there.
MATERIALS :
- Purify or clean the material because contaminated material can cause proper knitting of the material.
- Lubricate the material to make the material flow easily in the mold.


Comments
Post a Comment